
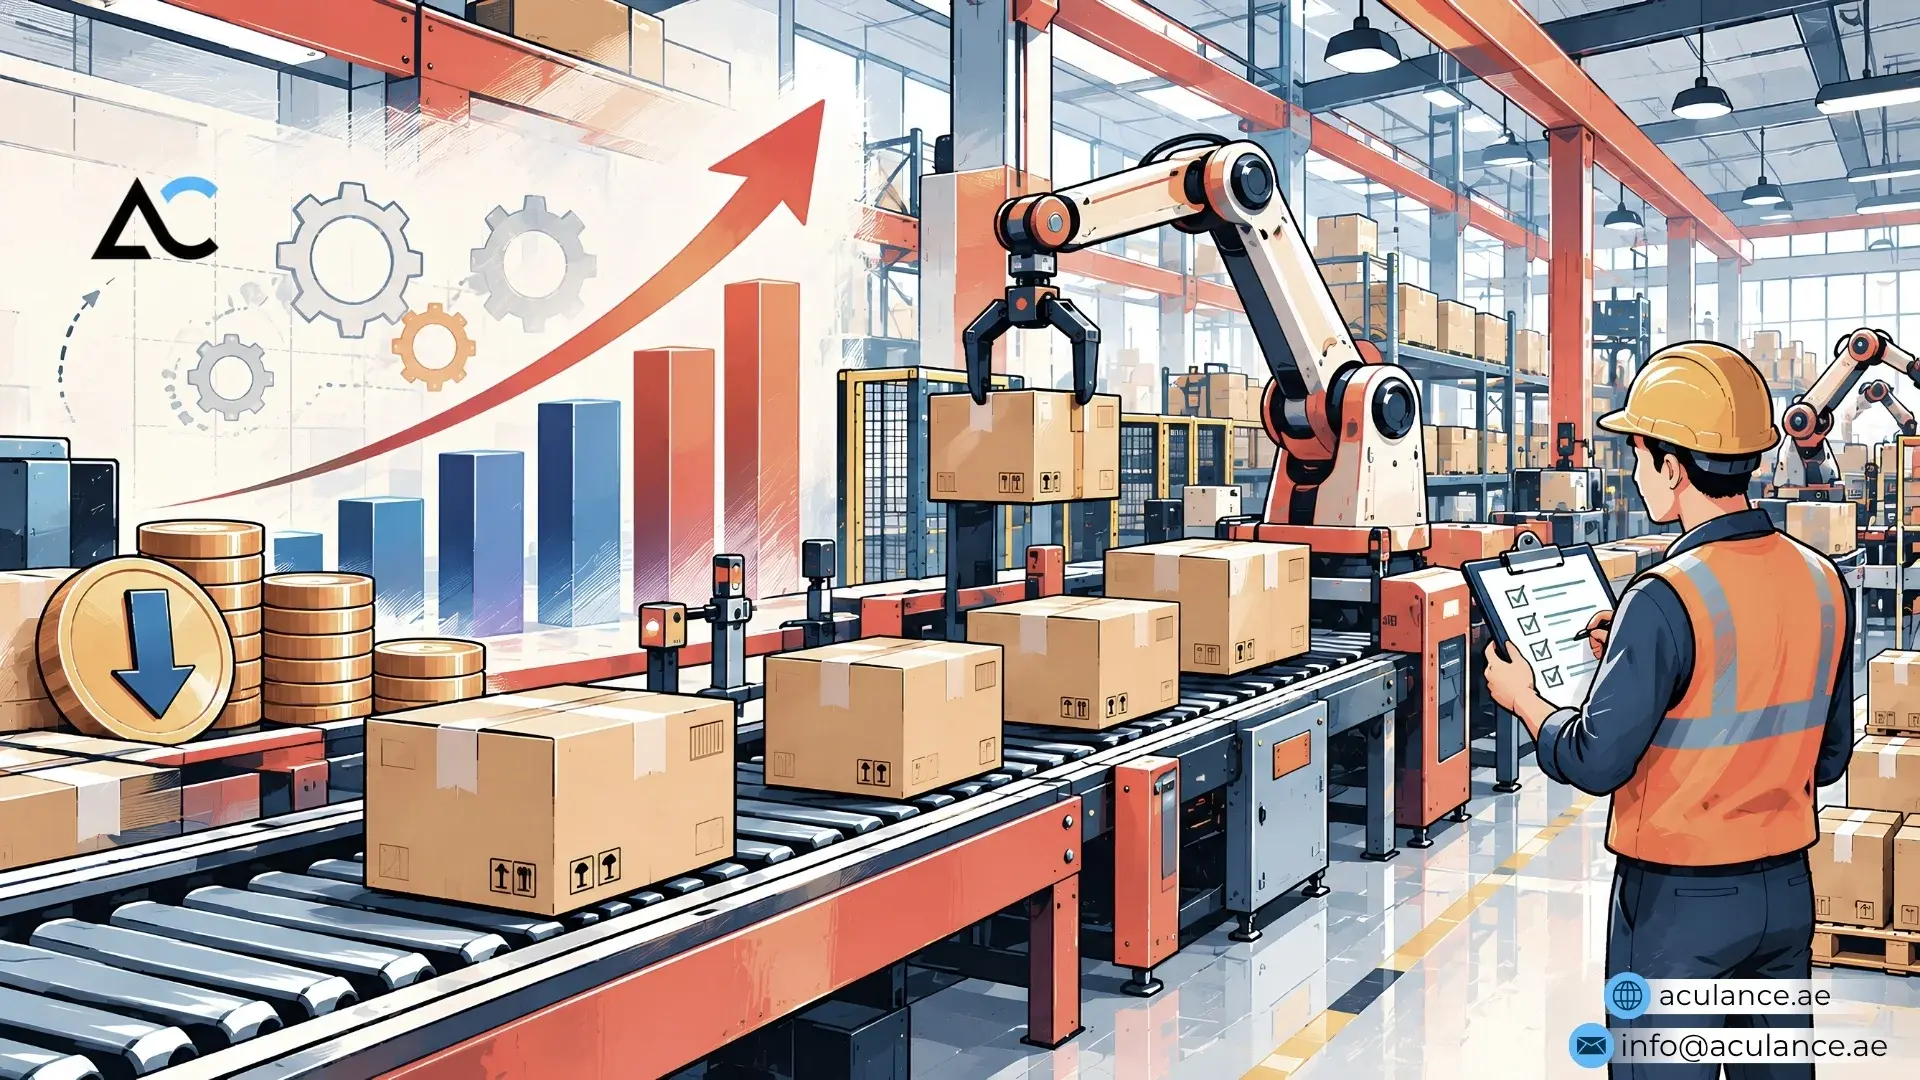
Manufacturing is no longer about simply producing more
It is about producing smarter, faster, and with fewer unexpected costs. Rising energy prices, equipment downtime, supply-chain disruptions, quality issues, and changing customer demand are putting manufacturers under constant pressure to improve operational efficiency.
This is where predictive analytics in manufacturing is becoming a strategic advantage.
Instead of waiting for a machine to fail or a quality problem to appear, predictive analytics uses historical data, real-time machine signals, artificial intelligence (AI), and machine learning (ML) to identify what is likely to happen next. This allows manufacturers to take
action before a small operational issue becomes an expensive disruption.
Modern manufacturing is also moving beyond standalone predictive maintenance. AI-powered analytics is increasingly being applied across production, quality, supply chains, energy, inventory, and workforce planning.
What Is Predictive Analytics in Manufacturing?
Predictive analytics in manufacturing combines data from sources such as IoT sensors, machines, ERP systems, MES platforms, maintenance records, quality systems, and production lines.
Machine learning models analyze this information to identify patterns, detect anomalies, estimate future outcomes, and recommend timely actions.
For example, instead of asking:
“Why did this machine stop yesterday?”
a predictive system can help answer:
“Which machine is likely to develop a problem next week, and what should we do about it?”
That shift from reactive to proactive decision-making is what makes predictive analytics valuable for modern factories.
10 Predictive Analytics Use Cases in Manufacturing
1. Predictive Maintenance to Prevent Unexpected Downtime
Unexpected equipment failure can disrupt production schedules, increase repair expenses, and create delivery delays.
Predictive maintenance analyzes signals such as vibration, temperature, pressure, power consumption, and operating cycles to identify early signs of equipment degradation.
Maintenance teams can then schedule repairs before a failure occurs.
The result? Less unplanned downtime, better asset utilization, fewer emergency repairs, and longer equipment life.
This remains one of the most practical applications of predictive analytics because the financial impact of avoiding even one major production stoppage can be significant.
2. Predictive Quality Control and Defect Prevention
Traditional quality inspection often identifies problems after products have already been manufactured.
Predictive analytics changes that approach by identifying the conditions that are likely to create defects.
Models can analyze production temperature, pressure, speed, material properties, machine settings, historical defects, and inspection results to predict quality deviations.
Operators can intervene earlier, reducing:
- Scrap and material waste
- Rework
- Product recalls
- Warranty claims
- Production losses
AI-powered quality analytics is particularly valuable in complex production environments where many variables influence the final product.
3. Demand Forecasting for Smarter Production Planning
Demand can change quickly because of customer behavior, market conditions, seasonality, and supply-chain disruptions.
Predictive analytics can combine historical sales, market trends, order patterns, inventory levels, and external variables to estimate future demand.
Manufacturers can use these forecasts to determine:
- How much to produce
- When to increase production
- Which products require priority
- How much raw material to order
Better forecasting reduces both excess inventory and stockout risks while helping factories align production with actual market demand.
4. Inventory Optimization
Holding too much inventory ties up working capital. Holding too little can stop production.
Predictive analytics helps manufacturers identify future material requirements based on expected demand, production schedules, supplier lead times, consumption patterns, and inventory movement.
Instead of maintaining large safety stocks “just in case,” manufacturers can move toward more data-driven inventory decisions.
This creates a healthier balance between availability and cost.
5. Predictive Supply Chain Risk Management
Manufacturing performance depends on more than what happens inside the factory.
A delayed supplier, transportation disruption, raw-material shortage, or sudden demand spike can quickly affect production.
Predictive models can identify supply-chain risks before they become operational problems by analyzing supplier performance, lead times, historical disruptions, inventory positions, and demand signals.
Manufacturers can then identify alternative suppliers, adjust purchasing plans, change production schedules, or increase selected inventory buffers.
The goal is not simply to react faster, it is to see the risk earlier.
6. Energy Consumption Optimization
Energy can represent a major operational expense, particularly for energy-intensive manufacturing processes.
Predictive analytics can study historical energy consumption, machine utilization, production schedules, weather conditions, and peak-demand patterns to forecast future energy requirements.
Manufacturers can use these insights to identify abnormal consumption, schedule energy-intensive processes more efficiently, and detect equipment that is consuming more power than expected.
This supports two goals at once: lower operating costs and more sustainable production.
Energy optimization is becoming increasingly important as manufacturers connect operational efficiency with sustainability targets.
7. Production Scheduling and Bottleneck Prediction
A production line can lose significant time because of poor scheduling, machine constraints, material shortages, or unexpected changes in demand.
Predictive analytics can evaluate historical production performance, machine availability, order priorities, cycle times, and resource constraints to forecast potential bottlenecks.
Production managers can then adjust schedules before congestion occurs.
This can improve throughput, reduce idle time, and make production planning more responsive.
The latest manufacturing AI trend is moving toward connecting prediction with recommendations and, where appropriate, automated operational actions.
8. Workforce and Resource Planning
People remain a critical part of manufacturing operations even as factories become more automated.
Predictive analytics can help estimate workforce requirements using production forecasts, shift patterns, productivity data, absenteeism trends, and expected workloads.
Managers can use these insights to allocate workers more effectively and reduce unnecessary overtime.
The emerging direction is not simply replacing workers with AI. Instead, manufacturers are increasingly using AI to help employees make faster and better operational decisions. Current industry discussions emphasize the importance of combining AI capabilities with human expertise and continuous workforce upskilling.
9. Predictive Spare Parts Management
A maintenance strategy is only as effective as the availability of the required spare parts.
If a critical component fails and the replacement is unavailable, an otherwise manageable maintenance event can become extended downtime.
Predictive analytics can estimate which components are likely to require replacement based on equipment condition, operating history, failure patterns, and maintenance schedules.
This helps manufacturers stock the right parts at the right time rather than maintaining unnecessarily large spare-part inventories.
It can reduce storage costs while improving maintenance response times.
10. Digital Twins and Predictive Production Optimization
One of the most exciting developments in predictive analytics in manufacturing is the integration of AI with digital twins.
A digital twin creates a virtual representation of a machine, production line, or manufacturing process. When combined with real-time operational data and predictive models, it can help manufacturers test possible scenarios before making changes on the physical production floor.
For example, manufacturers can evaluate how changing production parameters could affect throughput, equipment performance, energy consumption, or quality.
Recent research shows that digital twins are evolving from basic monitoring tools toward intelligent platforms combining sensing, simulation, AI reasoning, and human interaction.
How Predictive Analytics Helps Reduce Manufacturing Costs
The value of predictive analytics is not limited to better dashboards. Its real impact comes from improving decisions that directly affect operational costs.
Manufacturers can potentially reduce costs by:
- Preventing unexpected equipment failures
- Reducing scrap and rework
- Optimizing energy consumption
- Improving inventory levels
- Reducing emergency maintenance
- Increasing production throughput
- Improving workforce utilization
- Identifying supply-chain risks earlier
However, successful implementation depends on more than selecting an AI model. Data quality, system integration, governance, workforce skills, and the ability to embed predictions into daily workflows are critical. Research published in 2026 highlights the continuing gap between generating analytics insights and consistently translating them into operational action.
Why Predictive Analytics Matters for UAE Manufacturers
The UAE is actively accelerating industrial digital transformation through Industry 4.0 initiatives. The Ministry of Industry and Advanced Technology highlights AI, predictive maintenance, quality monitoring, production planning, energy optimization, and supply-chain efficiency as important areas for industrial technology adoption.
For UAE manufacturers, this creates a strong opportunity to combine factory data with AI-powered decision-making.
Companies investing in manufacturing software development UAE capabilities can build connected platforms that bring together IoT devices, ERP, MES, maintenance systems, analytics, and AI models in one operational ecosystem.
This is particularly relevant as the UAE continues to position advanced technology and smart manufacturing as key drivers of industrial competitiveness.
How to Get Started with Predictive Analytics
Manufacturers do not need to transform the entire factory overnight.
A better approach is to begin with one high-value problem.
Start by identifying an operational issue with measurable financial impact such as downtime, defects, energy waste, or inventory inefficiency. Then collect the relevant data, establish baseline KPIs, develop a focused predictive model, and measure the business outcome.
Working with experienced predictive analytics services providers can also help manufacturers connect data engineering, machine learning, software integration, and business strategy.
The next step is scaling successful pilots across production lines, plants, and business functions.
Building a Smarter Manufacturing Future
Predictive analytics is changing manufacturing from a reactive environment into a more proactive and intelligent operation.
From predicting machine failures and preventing defects to forecasting demand, optimizing energy, managing inventory, and powering digital twins, its applications extend across the entire manufacturing value chain.
The competitive advantage will not simply belong to factories with the most AI technology. It will belong to manufacturers that can turn data into timely decisions and measurable operational improvements.
For organizations exploring predictive analytics services or investing in manufacturing software development UAE, the opportunity is clear: start with a business problem, prove measurable value, and build toward a connected, intelligent manufacturing ecosystem.
Get a Predictive Analytics Consultation
Frequently asked questions
What is predictive analytics in manufacturing?
Predictive analytics in manufacturing uses historical data, real-time machine signals, AI, and machine learning to predict future outcomes and help manufacturers make proactive decisions. Pasted markdown
What are the top predictive analytics use cases in manufacturing?
Key use cases include predictive maintenance, quality control, demand forecasting, inventory optimization, supply chain risk management, energy optimization, production scheduling, workforce planning, spare parts management, and digital twins. Pasted markdown
How does predictive analytics reduce manufacturing costs?
It can reduce costs by preventing equipment failures, minimizing scrap and rework, optimizing energy consumption, improving inventory levels, reducing emergency maintenance, increasing production throughput, and identifying supply-chain risks earlier. Pasted markdown
How does predictive maintenance improve manufacturing efficiency?
Predictive maintenance analyzes machine data such as vibration, temperature, pressure, and power consumption to identify early signs of equipment problems, allowing manufacturers to schedule maintenance before unexpected failures occur. Pasted markdown
How can manufacturers get started with predictive analytics?
Manufacturers can start by identifying one high-value problem, such as downtime, defects, energy waste, or inventory inefficiency, then collect relevant data, establish KPIs, develop a focused predictive model, and measure the results before scaling. Pasted markdown